Automated Dispensing Robot Videos

A World of Robotic Dispensing and Assembly Solutions

How to Choose a Hydraulic Forging Press?

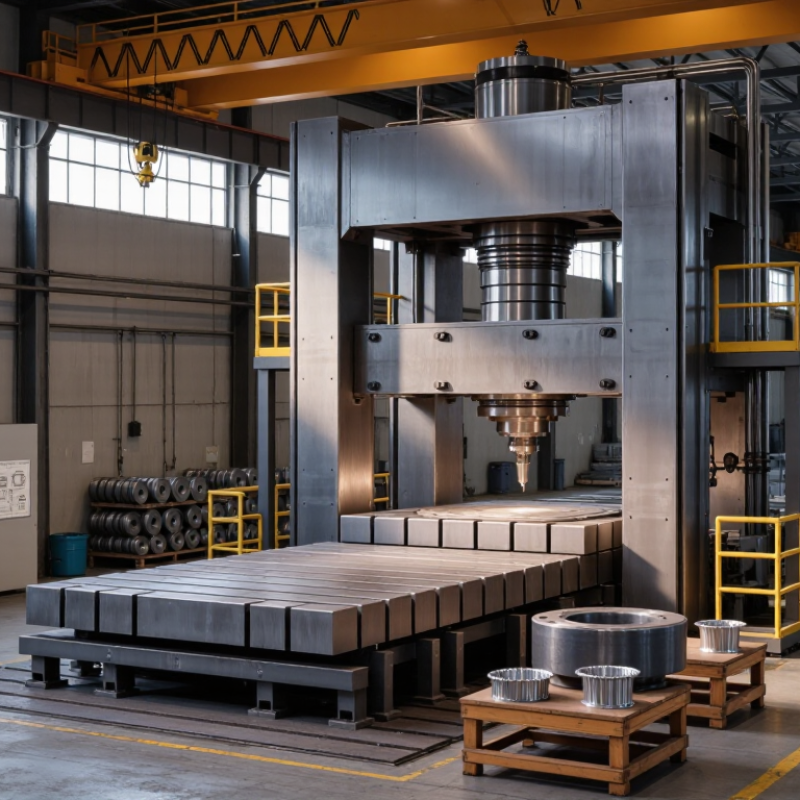
Choosing a Hydraulic Forging Press begins with the part, not the machine’s headline tonnage. Forgings differ in alloy, shape, temperature, and production volume. A press suited to a small aluminum component may struggle with a large steel die. That mismatch costs time.

The scale is substantial. World Steel Association data reports that global crude steel production reached about 1.89 billion tonnes in 2023. Steel output is not a direct measure of forging demand, but it shows the size of the material supply chain behind many forged products. Grand View Research’s global forging market analysis also identifies automotive applications as a major market segment. These reports offer context, not a press specification. Actual requirements must come from the component and process.

Start with the forging force required, then check stroke, daylight, bed dimensions, and operating speed. Match these figures to the largest workpiece and the die set, leaving practical space for handling. Ask suppliers for load curves, cycle estimates, and service requirements—not just a capacity number. In real production, a press that meets tonnage on paper can still fall short if its stroke or control response is unsuitable. Details matter.

There is no perfect shortcut. Compare hydraulic systems, controls, safety features, maintenance access, and energy use against your operating plan. Test assumptions with sample parts or process data where possible. A cautious choice may feel slower, but replacing an undersized press is slower still. The right machine is the one that can produce the required forging reliably, at the planned rate, with room for realistic variation.

How to Choose a Hydraulic Forging Press?

Define the Forging Requirements and Workpiece Range

Define the actual work before comparing press tonnage. Record the alloy, forging temperature, finished dimensions, billet size, part weight, tolerances, and annual volume. Include the smallest and largest workpieces, not just the most common one. A press that handles a large shaft may still struggle with a thin, wide component. It can also waste energy and floor space on small parts.

Material changes the load. ASM Handbook, Volume 14A: Metalworking: Bulk Forming, gives typical hot-forging temperature ranges of about 900–1,250°C for steels and 350–500°C for aluminum alloys. These are reference ranges, not production settings; the specific alloy and process matter. Use the workpiece’s projected area, deformation resistance, temperature, and die friction to estimate forming force. Then check stroke, daylight, table size, and ejector capacity against the largest die setup. Check them again against the smallest part. Easy to miss. Leave practical room for handling and die changes, but avoid sizing around an unlikely future job. I would verify estimates with trial data; calculations alone can be optimistic, especially when material temperature varies across a billet.

How to Choose a Hydraulic Forging Press?

Define the Forging Requirements and Workpiece Range

Use the workpiece’s projected area—the surface area under compression—to make an initial press-capacity estimate. The ranges below are illustrative planning values for hot-steel forging, based on an assumed forging pressure of 0.6–1.2 metric ton-force per cm² plus a 20% allowance. Actual force depends on material, temperature, geometry, dies, and process conditions.

Selection tip: Treat this chart as a preliminary guide. Confirm peak force, force at the required stroke, energy, daylight, stroke, and die dimensions with a forging-process engineer before selecting a press.

Calculate the Required Press Capacity and Operating Pressure

Estimate the forging load from the part’s projected area and the material’s flow stress at the planned forging temperature. Add allowance for shape complexity, die friction, and the deformation rate; a simple area calculation can understate the real load. Small details matter. Use material data that matches your process, not room-temperature figures.

Then convert the estimated load into press capacity. Hydraulic force is approximately operating pressure multiplied by the total effective piston area. For example, a 300 mm bore has an area of about 0.0707 m²; at 25 MPa, it produces roughly 1.77 MN, or 180 metric tonnes-force, before losses. Check the units. Account for cylinder count and efficiency, and select capacity with a suitable engineering margin rather than treating the estimate as an exact limit.

Choose the cylinder area and pressure together. A larger bore can deliver the required force at lower pressure, but it may need more oil flow to maintain stroke speed. Set operating pressure to meet the load during the working stroke, while staying within the ratings of the cylinder, hoses, valves, and frame. The estimate is not a promise: billet temperature, lubrication, and die condition vary. Confirm the setup with pressure readings and controlled production trials.

Choose the Frame Design, Stroke, and Working Space

How to Choose a Hydraulic Forging Press?

Choose the Frame Design, Stroke, and Working Space

Frame design sets the press’s stiffness and access. A four-column frame offers open access from several sides, while a closed-frame design can provide greater rigidity under heavy loads. Match the frame to the workpiece and tooling, not just the rated tonnage. A press that deflects can produce uneven dies and inconsistent parts. Check the manufacturer’s load-deflection data and confirm where the force is measured.

Stroke and working space must suit the full production sequence. Measure the billet, die height, and required loading clearance. Then allow room for the ram to approach, form, and retract without slowing handling. World Steel Association’s World Steel in Figures 2024 reports 1,892.2 million tonnes of crude steel production in 2023. That figure reflects the scale and variety of steel production, but it cannot determine your press size; actual material grade and part geometry matter. I’ve seen clearance treated as an afterthought. It shouldn’t be.

Compare Hydraulic Systems, Controls, and Automation Options

Compare the hydraulic circuit and controls as one production system, not as separate quotations. A variable-displacement pump may reduce idle losses, while servo-hydraulic control can match flow to changing press demand. Verify both against actual tonnage, stroke, and duty cycle. Ask for oil-temperature, energy-per-part, and cycle-time readings under your tooling. Watch the return stroke: poor recovery can erase gains.

The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, up 10% from 2022, in World Robotics 2024. That figure covers all industries, not forging alone, but it shows automation is scaling. For a forging line, compare options such as billet loading, part removal, and transfer between operations. Check how the press handles interruptions and whether operators can safely intervene.

Controls should record force, position, alarms, and recipe changes. This makes drift easier to investigate when a die warms or material varies. Ask to see a sample production record, not just a control-screen demonstration. There is no perfect configuration. A sophisticated system can add maintenance and training burdens, so weigh its promised output against the skills available on your floor.

Evaluate Safety Features, Maintenance Needs, and Supplier Support

How to Choose a Hydraulic Forging Press?
Evaluate Safety Features, Maintenance Needs, and Supplier Support

A press should suit both the forging task and its operators. Check rated force across the full stroke, not only the headline tonnage. Confirm usable daylight, stroke length, bed dimensions, and cycle rate against actual dies and heated workpieces. Inspect fixed guards, interlocked access points, emergency stops, pressure-relief protection, and control layout. Ask how the press responds to power loss or sensor failure. Small details matter. A guard can obstruct die changes, so include operators in the review.

Maintenance affects the press’s real cost of ownership. Look for accessible filters, labeled hydraulic lines, safe service access, and clear oil-check procedures. Ask which service intervals assume your daily cycles and shop conditions. A brochure rarely captures dust, heat, or hurried shift changes. That gap deserves attention. Confirm technician availability, realistic response times, spare-parts access, operator training, and service documentation before purchase. A clean specification sheet can still leave practical questions unanswered.

Tips: Bring a sample die and typical workpiece to the technical review. Request a maintenance checklist and written support plan. Compare specific answers, not promises; unclear service expectations can mean longer stoppages.

How to Choose a Hydraulic Forging Press? — Evaluate Safety Features, Maintenance Needs, and Supplier Support

Evaluation Area What to Check Evidence to Request or Verify Selection Guidance
Press capacity Rated force, working pressure, and the force available throughout the required stroke. Capacity chart showing force versus stroke or operating conditions; confirm the rating matches the intended forging process. Choose a press with adequate capacity for the actual workpiece and process, without relying on peak force alone.
Die space and stroke Daylight, stroke length, bed dimensions, and space for dies, tooling, and workpiece handling. General arrangement drawing with the working envelope, bed size, daylight, stroke, and any relevant openings. Check the largest planned die and workpiece, plus the clearance needed for loading and maintenance.
Operating speed and control Approach, working, and return speeds; cycle control; and the ability to adjust the process where required. Cycle description and speed data for the intended operating mode; confirm control functions and operator interfaces. Match the speed profile to the forging process and required production rate, not just the fastest stated cycle.
Point-of-operation safety Protection against access to the die area during hazardous motion, including guarding and interlocked access where appropriate. Risk assessment, safeguarding layout, safety-control documentation, and a demonstration of protective functions. Assess the complete installation and operating method against applicable local safety requirements.
Emergency and safety controls Emergency-stop access, safe stopping behavior, control reliability, and protection against unexpected restart. Safety circuit information, stop-function test procedure, restart procedure, and instructions for lockout and isolation. Confirm operators can reach controls safely and that maintenance isolation procedures are clearly documented.
Hydraulic system Pump and motor arrangement, filtration, fluid cooling, leak control, and monitoring of pressure and temperature. Hydraulic schematic, recommended fluid and filtration requirements, inspection points, and alarm or monitoring details. Prefer an accessible layout with clearly identified service points and suitable provisions for the operating environment.
Routine maintenance Inspection intervals and service tasks for hydraulic fluid, filters, hoses, seals, guides, and electrical components. Maintenance schedule, parts list, lubrication instructions, and estimated routine service requirements. Compare the workload and service access with the skills and maintenance resources available at your facility.
Wear parts and spares Availability of filters, seals, hoses, sensors, and other parts that may need replacement during service life. Recommended spare-parts list, part identification information, typical availability, and ordering process. Check lead times for critical items and identify suitable spares before commissioning.
Installation and utilities Foundation loads, floor requirements, electrical supply, hydraulic cooling needs, and space for installation and service. Installation drawings, utility requirements, shipping and handling details, and commissioning checklist. Confirm site readiness, access routes, and utility capacity before finalizing the equipment configuration.
Supplier support Installation assistance, operator and maintenance training, technical response, and service coverage. Written scope of supply, training plan, warranty terms, service contact process, and support response commitments. Compare support commitments in writing and confirm they cover the intended location and operating schedule.
Acceptance and documentation Factory and site acceptance checks, operating instructions, safety information, drawings, and maintenance records. Proposed acceptance-test checklist and complete documentation package in a language the operating team can use. Agree on measurable acceptance criteria before purchase and retain records for training and future servicing.
Practical tip: Compare presses using the same workpiece, die dimensions, production assumptions, and safety requirements. Confirm final machine specifications and safeguarding with a qualified engineering professional for the intended installation and jurisdiction.